
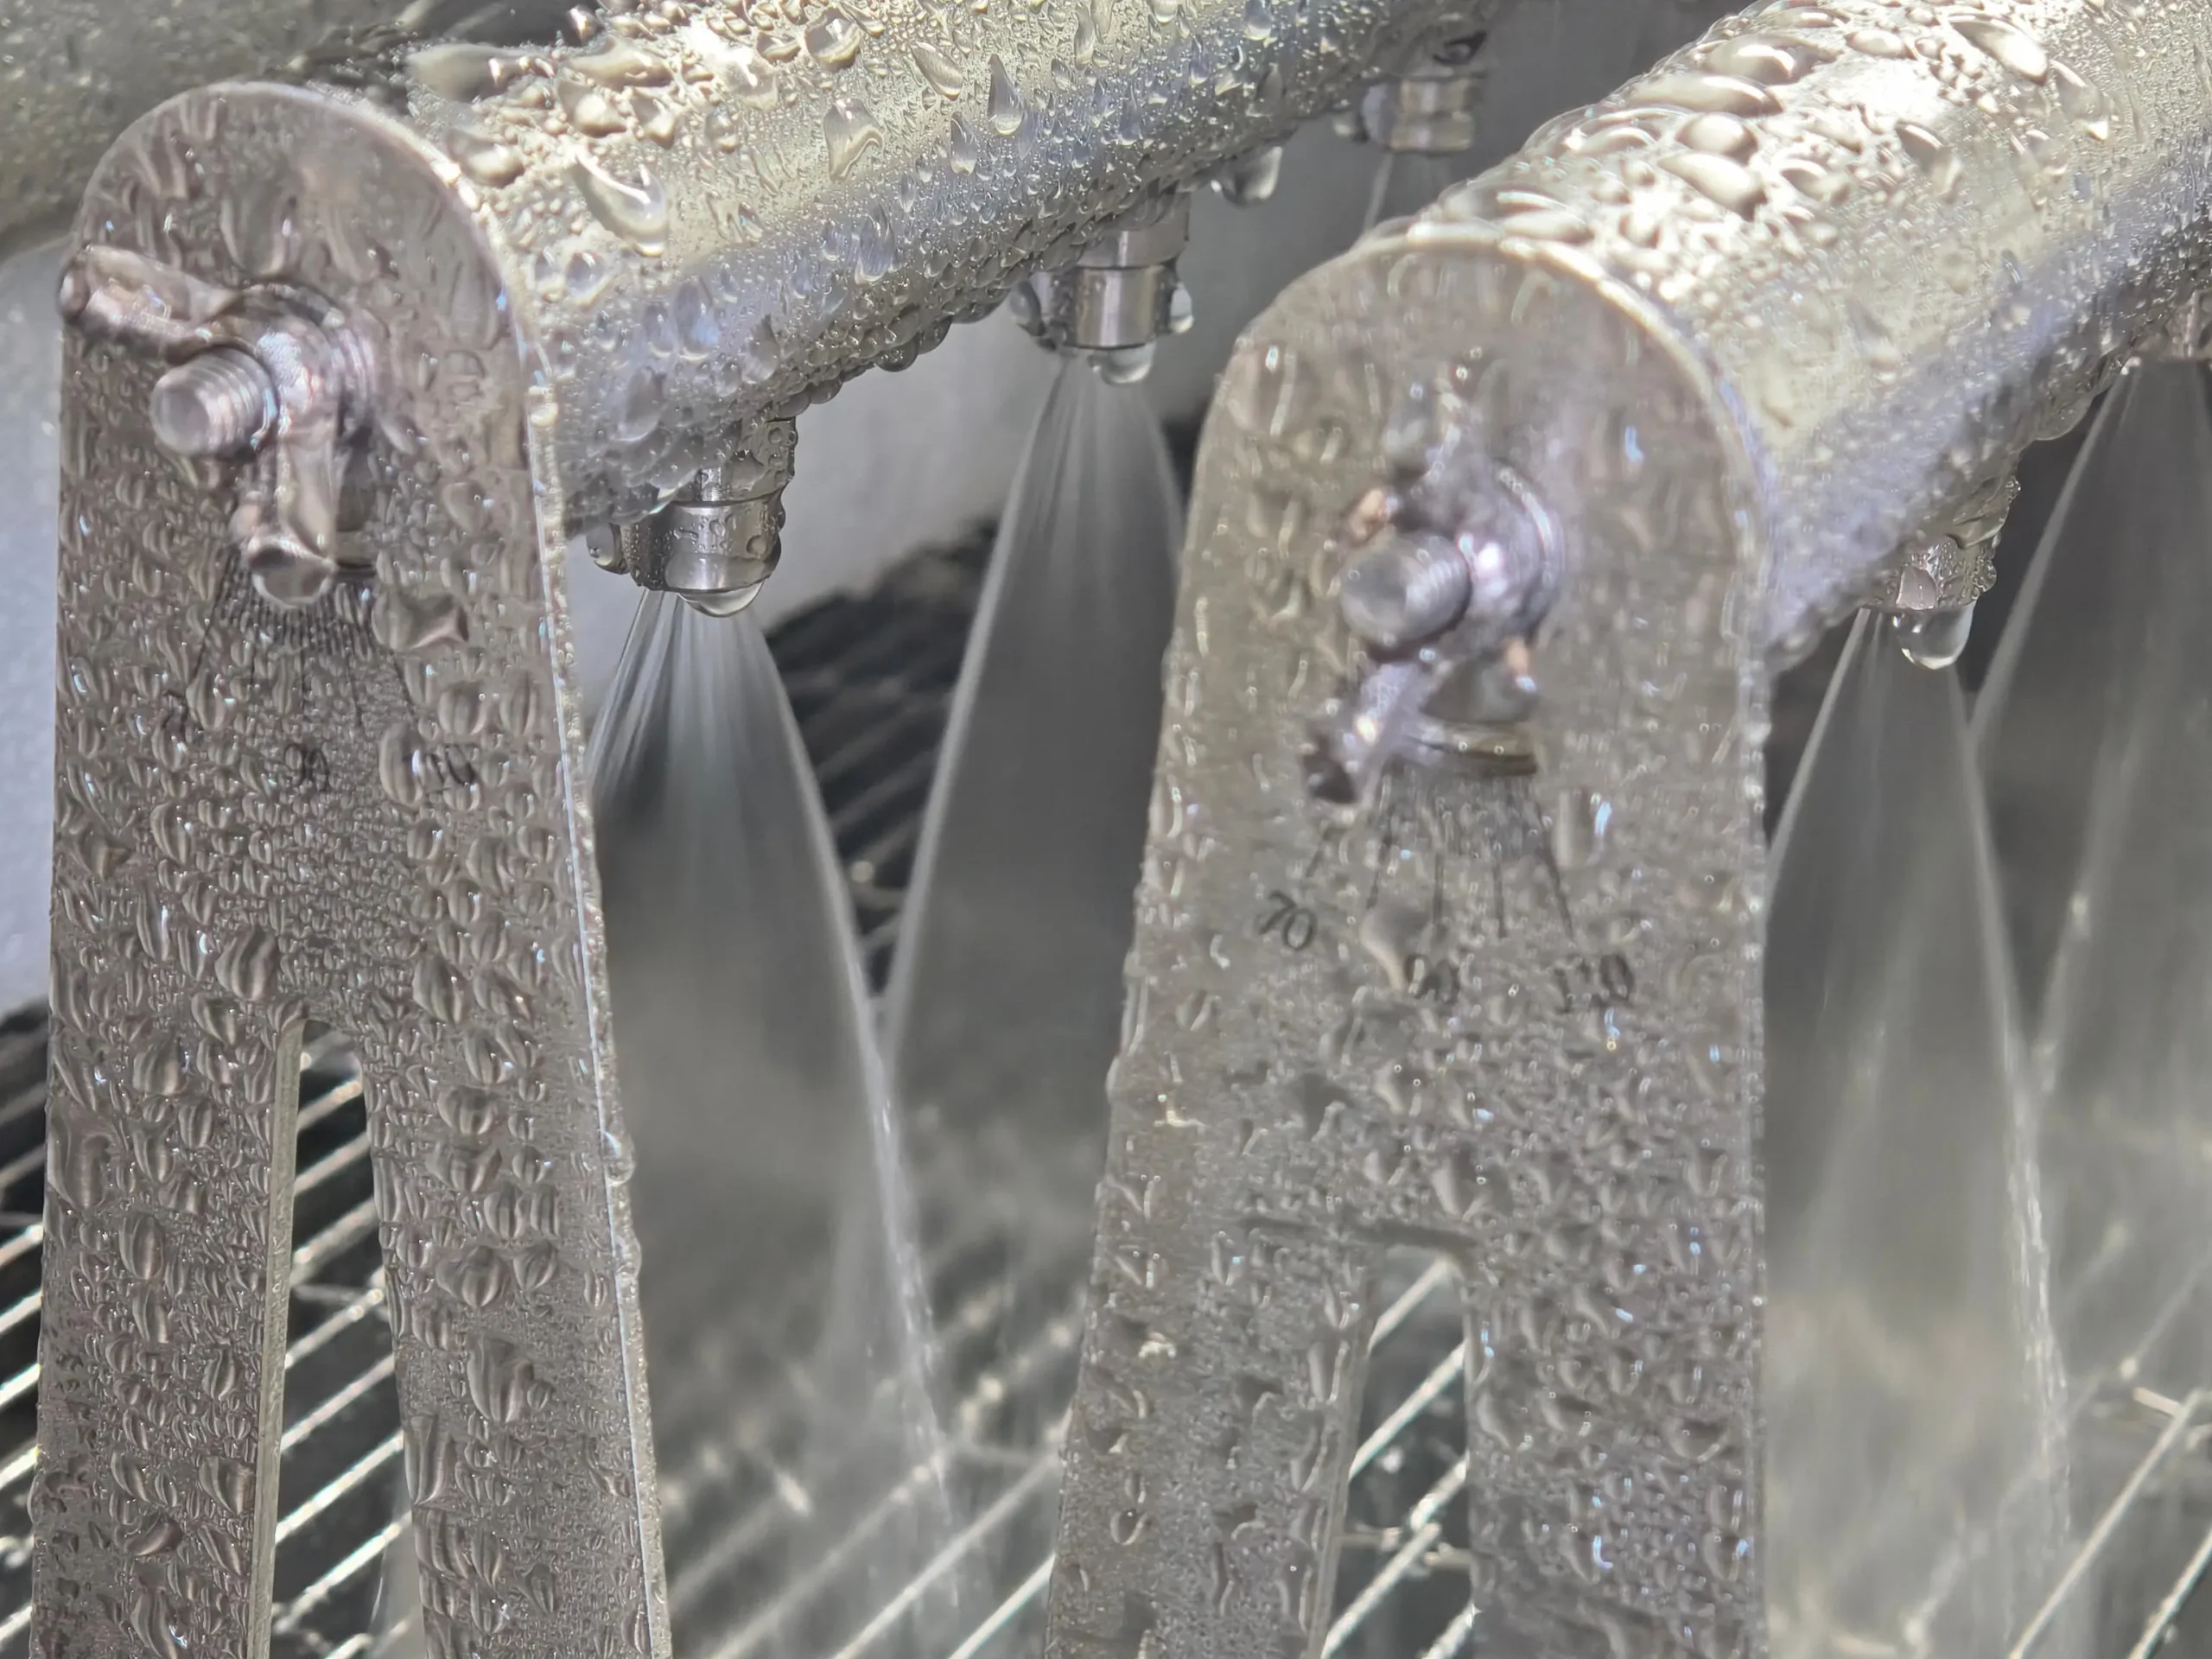
The cleaning machine is running exactly as specified. Wash temperature is on target, conveyor speed is unchanged, chemistry concentration was checked this morning. Yet ionic contamination readings drift upward through the shift, and every few hundred boards the test results look like the rinse stage stopped working.
The water in the rinse tank is clear. That is the problem: it looks clean enough that nobody treats it as a process variable.
Water Is a Process Chemical Too
In aqueous PCBA cleaning, chemistry does the work of lifting residue. Water is what carries it away. If the water arriving at the final rinse already carries ions, organics, or particles, the board does not finish clean—it finishes with a thin film of whatever was in the water.
That film is invisible. It shows up later as a failed ionic contamination test, a white mark after drying, leakage under bias, or a coating that lifts at the edges. The wash stage gets blamed, the chemistry gets replaced, and the actual variable stays untouched.
What “Clean Water” Actually Means
Water quality in a cleaning line is not a single number. Several failure modes share the same clear appearance:
- Conductivity and resistivity drift. Deionized water loses resistivity as it absorbs gases from air, sits in a tank, or travels through a long distribution loop. A reading taken at the generator says nothing about the water arriving at the spray nozzle.
- Ion exchange exhaustion or RO decline. Resin beds and membranes degrade gradually. There is usually no alarm at the moment performance crosses the line that matters for your process.
- Total organic carbon. Organic contamination does not always move conductivity much, but it leaves residue on the board and can interfere with coating adhesion.
- Particles and biological growth. Dead legs, stagnant lines, and warm tanks support biofilm. Particles settle on wet boards and stay there after drying.
- Cross-contamination from the wash stage. Carryover overwhelms the rinse if flow, pressure, or overflow rate is insufficient. No water system can compensate for a rinse stage that is hydraulically undersized.
Clear water tells you it is not visibly dirty. It does not tell you what is dissolved in it.
What You See vs. What to Check
| Symptom | Common assumption | Check this first |
| Ionic contamination rising after washing | Wash chemistry too weak | Final rinse resistivity at the point of use |
| White residue after drying | Drying temperature too low | Dissolved solids in the last rinse stage |
| Corrosion on connectors after storage | Board handling or packaging | Chloride and ionic carryover in rinse water |
| Readings differ between shifts | Test method inconsistency | Tank turnover, water system recovery cycles, dead legs |
| Coating adhesion varies by board position | Coater settings | Rinse coverage and water quality at the far nozzles |
| Water test passes but board test fails | Measurement error | Sampling point and contact time during extraction |
The Water System Is Part of the Cleaning Machine
Treating the DI water generator as a separate utility is a category error. It is part of the cleaning process and should be specified, monitored, and maintained with the same discipline as the washer itself.
Practical points that matter on a production line:
- Measure at the point of use, not only at the generator outlet. Distribution piping, storage tanks, and branch lines change the water before it reaches the board.
- Control storage time. Water held in a tank picks up contamination. Turnover matters more than tank size.
- Watch the return loop. If rinse water is recovered and recirculated, contamination accumulates upstream of the point where you take your sample.
- Include the weakest nozzle. Water quality is only useful if the water actually reaches the board surface at every position on the conveyor.
- Set an action limit, not just a target. Define what happens when resistivity drifts below the process threshold: pause, divert, regenerate, or reject.
A DI Water Generator Machine sized for the washer’s real consumption—not for an average number on a datasheet—is the difference between a rinse that resets the board and a rinse that re-contaminates it.
Wastewater Treatment Is Not Just Compliance
Rinse wastewater treatment is usually justified on environmental grounds, which is correct but incomplete. It also protects process stability.
An unstable treatment system creates variable makeup water. Variable makeup water feeds the DI system. The DI system drifts, and the board sees the drift before any instrument alarm does. Treatment that is designed only to meet discharge limits, without regard to how it feeds back into the cleaning loop, leaves the washing process exposed to every upstream disturbance.
Treat the wash, rinse, water generation, and wastewater handling as one system with one owner and one set of measured handoffs.
A Water Quality Checklist for PCBA Washing
- Point-of-use resistivity or conductivity logged per shift, with defined action limits
- Regular checks for organic load, not only ionic readings
- Inspection of storage tanks, filters, and dead legs on a fixed schedule
- Verification of rinse flow, overflow, and coverage across the full conveyor width
- Documented resin or membrane maintenance tied to measured performance
- Makeup water quality reviewed as part of wastewater system performance
- Board cleanliness verified independently of water readings
Measure the Board, Not Just the Water
Water monitoring tells you whether the rinse system is behaving. It does not tell you whether the board is clean. Those are different questions and both need answers.
An Ion Contamination Tester on the line closes the loop. When water quality drifts, the board test catches the consequence. When the board test fails, water data helps you find the cause. Neither one alone is enough to control the process.
The production managers who keep washing under control are the ones who stopped treating water as a free, invisible input. It is a chemical, a cost, and a reliability variable—in that order.
FAQ
Can rinse water that looks clear still contaminate a board? Yes. Dissolved ions, organics, and fine particles are invisible and can leave a residue film after drying. Clear appearance is not a cleanliness specification.
Where should water quality be measured for a cleaning line? At the point of use, at the final rinse stage. Generator outlet readings do not account for storage tanks, distribution loops, or contamination picked up along the way.
Does a DI water generator alone guarantee a good rinse? No. Generator capacity, storage time, distribution losses, rinse hydraulics, and carryover from the wash stage all affect the water that actually reaches the board.
How do I connect water quality to board cleanliness? Log water parameters per shift and verify boards with ionic contamination testing. Correlate the two. When they move together, you have a controllable process instead of a recurring mystery.
About ACTSPRAY
ACTSPRAY (Dongguan, Guangdong, China) develops and manufactures precision cleaning equipment for microelectronics, with spray, ultrasonic, jet flow, and vacuum, plus non-standard custom systems.
- PCBA Cleaning Machine: Inline & Offline PCBA Cleaning Machine, PCBA Pure Water Washer, DI Water Generator Machine, Rinse Wastewater Treatment Machine, Ion Contamination Tester.
- Semiconductor Packaging Cleaning Machine: FlipChip Cleaner / SIP Cleaner / BGA Solder Ball Cleaner / PLP Cleaner / Leadframe Cleaner / Power Module Cleaner / IC Substrate Cleaner / Carrier Cleaner and JEDEC Tray Cleaner.
- SMT Cleaning Machine: Stencil cleaner, wave soldering fixture cleaner, reflow oven condenser cleaner, squeegee blade cleaner, PCB magazine cleaner.
If you are evaluating whether residue is behind intermittent solder or reliability issues, our team can help match the cleaning process and cleanliness verification method to your specific assembly.